CNC Reaming Kovar is a core capability at VT machining. We combine controlled machining with material-aware setup for Kovar — an alloy that is matched thermal expansion for glass/ceramic seals — to produce parts that meet your specification first time.
Starting Parameters for CNC Reaming Kovar
| Cutting speed (carbide) | 10-25 m/min |
|---|---|
| Stock allowance on Ø10 mm | 0.15-0.25 mm |
| Feed | 0.09-0.288 mm/rev |
| Spindle speed, Ø10 mm | 320-800 rpm |
| Insert / tool class | ISO S — sharp PVD-coated carbide |
| Coolant | Flood emulsion; sulphurised oil for tapping |
Shown for Kovar, the most common Kovar grade we see for CNC Reaming. Starting values for Kovar, Annealed; optimised on the first article.
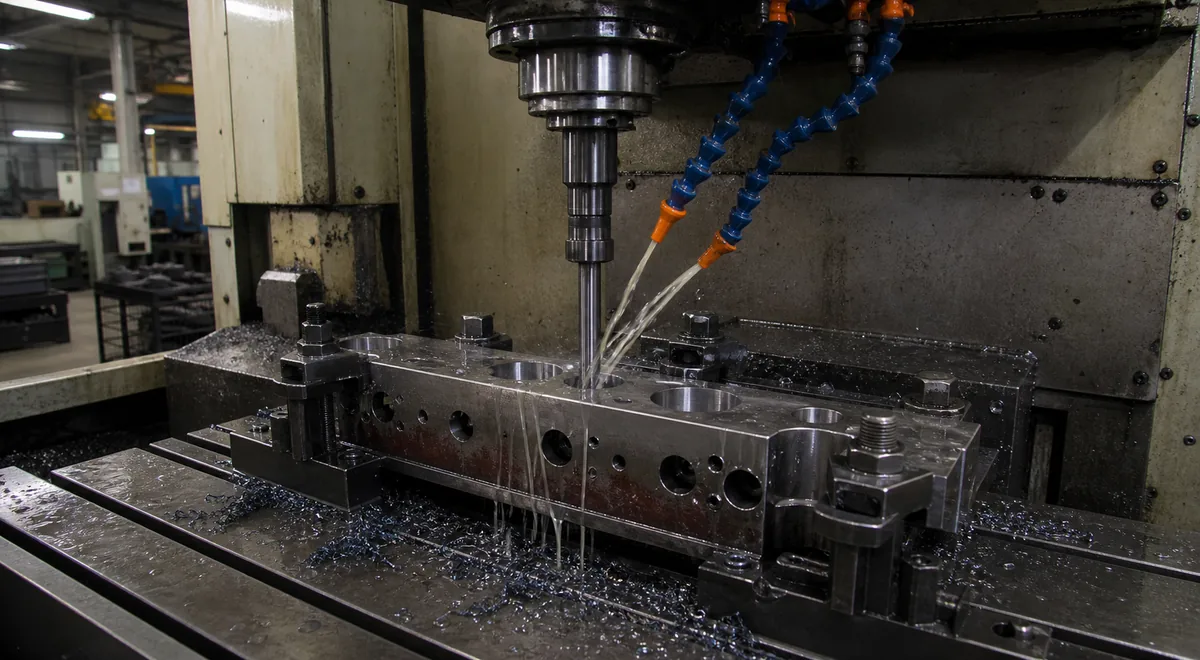
CNC Reaming Capability for Kovar
- H7 hole tolerance typical
- Ra to 0.4 µm bore finish
- Carbide and HSS reamers
- Pilot-guided accuracy
Kovar material properties, finishing options and grade notes are on our CNC Milling Kovar page.
How CNC Reaming Kovar Works
Rotating multi-flute cutters remove material as the Kovar workpiece is driven through programmed tool paths on 3-, 4- or 5-axis machining centres. Climb milling, step-over and depth-of-cut are set so chip load stays in the ideal band for the alloy.
We start from your supplied geometry and tolerance scheme. The setup is designed to minimise re-clamping, which protects positional accuracy across features. A first article is verified against the drawing before the balance of the batch is released.
Achievable Tolerances for CNC Reaming Kovar
| Feature | Standard | Precision |
|---|---|---|
| Linear dimension (< 100 mm) | ±0.05 mm | ±0.010 mm |
| Linear dimension (100–300 mm) | ±0.10 mm | ±0.025 mm |
| Hole diameter (reamed) | H9 | H7 |
| True position of hole pattern | ±0.10 mm | ±0.025 mm |
| Flatness over 100 mm | 0.05 mm | 0.015 mm |
| Perpendicularity | 0.10 mm | 0.020 mm |
| Surface finish, as machined | Ra 1.6 µm | Ra 0.4 µm |
Standard is what a normal quotation assumes. Precision is available on nominated features and is priced separately, because it needs extra setups, in-process gauging and CMM verification. Call out only the features that need it — blanket-tightening a drawing is the single most common reason a quote comes back expensive.
CNC Reaming Tolerances & Surface Finish
For CNC Reaming, dimensional and positional tolerances around ±0.01 mm are routine, tightening toward ±0.005 mm on precision setups. Surface finish on machined faces typically falls in the Ra 0.4–1.6 µm range depending on tooling and pass strategy.
The tightest tolerances are reserved for the features your drawing flags as critical. Share your tolerance scheme and we will confirm what is realistic before quoting.
Design Tips for CNC Reaming Kovar
Small design adjustments often cut cost and lead time. Generous internal radii, sensible pocket depth-to-width ratios and avoiding very thin unsupported walls all reduce cost and improve accuracy in Kovar. If you send your model early, we will return practical DFM feedback before you commit to production.
Applications of CNC Reaming Kovar
Kovar parts made this way are found throughout aerospace, medical, automotive, electronics and industrial equipment. Prototype, bridge and production volumes are all welcome.
Typical Kovar Parts for CNC Reaming
Illustrative examples of CNC Reaming Kovar parts and the callouts that usually drive the process plan. They show the kind of work that fits this process; they are not specific customer orders.
Heat sink base
- Material
- Kovar
- Size
- 200 × 100 × 8 mm
- Key callouts
- Fin thickness 1.2 ±0.05 mm, base flatness 0.03 mm
- Batch
- 500 pcs
Fins cut with a slotting cutter in one pass to avoid the deflection a step-over leaves.
Manifold block
- Material
- Kovar
- Size
- 120 × 60 × 45 mm
- Key callouts
- Cross-bore intersection ±0.05 mm, ports G1/8", leak-tested to 10 bar
- Batch
- 80 pcs
Deburred internally with a brush tool; a burr at a cross-bore is what fails the leak test.
Robot end-effector bracket
- Material
- Kovar
- Size
- 180 × 90 × 30 mm
- Key callouts
- Bore pair concentric within 0.02 mm, weight reduction pockets
- Batch
- 120 pcs
Pockets ganged so wall thickness never drops below 2 mm at the load path.
No drawing yet? Build one in the browser.
Set the metal, dimensions and features, watch the 3D model update as you type, then switch to the 2D sheet to add dimensions and tolerances. Download it or send it straight to us with your RFQ.
What We Need to Quote CNC Reaming Kovar
- GeometrySTEP or IGES for the 3D model, plus a PDF drawing if you have tolerance callouts. A dimensioned sketch is enough to start.
- MaterialThe exact Kovar grade and condition — temper, heat-treat state or hardness. If you are not sure, tell us the function and we will suggest one.
- QuantityPrototype count and the expected annual volume. Both change how the part is made and therefore what it costs.
- TolerancesWhich features are critical. Everything else runs to our standard tolerance, which is what keeps the price sensible.
- FinishSurface treatment, cosmetic requirements, and any faces that must be masked.
- DocumentsWhether you need a material certificate, dimensional report, FAIR or PPAP with the shipment.
Missing something from the list is not a problem — send what you have. We will come back with the specific questions rather than a generic form.
Other Metals for CNC Reaming
Other Processes for Kovar
Send the drawing, the Kovar grade and the quantity. You get pricing, lead time and any DFM notes back — usually within one business day.
Request a QuoteFrequently Asked Questions
Which industries use CNC Reaming Kovar parts?
CNC Reaming Kovar parts are used across aerospace, medical, automotive, electronics, semiconductor and general industrial sectors — anywhere precise Kovar components are required.
How clean are the edges produced by CNC Reaming on Kovar?
Machined Kovar edges are clean and to specification; edge-break or deburring is added when your drawing calls for it.
What surface finish is achievable on Kovar with CNC Reaming?
Surface finish on Kovar is controlled to your specification; we confirm the achievable Ra against your callout.
What is the typical lead time and minimum order for CNC Reaming Kovar?
CNC Reaming prototypes for Kovar can be produced quickly and scaled to series production. Send your drawing and quantity and we will advise lead time and any minimum order.