VT machining provides CNC Cylindrical Grinding Hard Alloys for customers who need accurate, repeatable Hard Alloys components. Because Hard Alloys is wear-resistant carbide and hardened tool materials, we adapt the process to suit — controlling the variables that matter for this alloy.
Process Data for CNC Cylindrical Grinding Hard Alloys
| Wheel (supply condition) | Diamond (resin or metal bond) |
|---|---|
| Depth per pass (rough / finish) | 0.005-0.015 / 0.002-0.005 mm |
| Achievable finish | Ra 0.1-0.2 µm |
| Typical size tolerance | Ø ±0.002 mm, roundness 0.001-0.002 mm |
| Diameter growth, Ø50 mm, +3 °C | 0.8 µm |
| Work speed | 15-30 m/min (between centres) |
Shown for Tungsten Carbide, the most common Hard Alloys grade we see for CNC Cylindrical Grinding. Typical values for Tungsten Carbide, Sintered; confirmed on the first part.
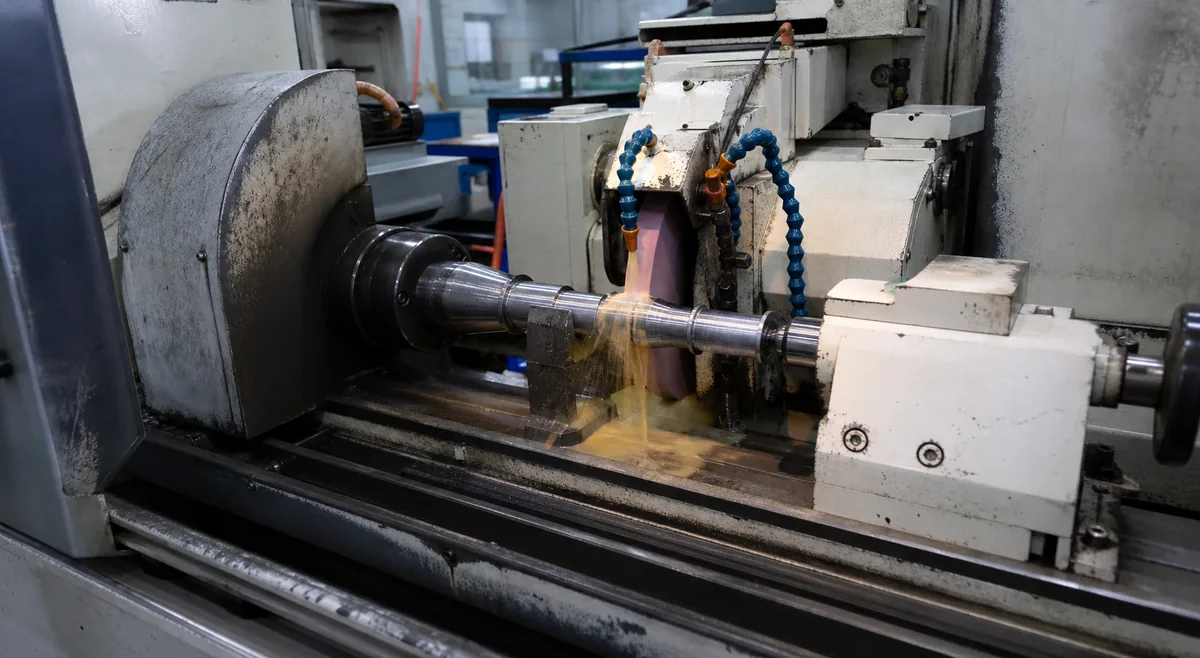
CNC Cylindrical Grinding Capability for Hard Alloys
- Roundness within 0.002 mm
- OD tolerance ±0.002 mm
- Ra to 0.2 µm
- Between-centers work
Hard Alloys material properties, finishing options and grade notes are on our CNC Surface Grinding Hard Alloys page.
How CNC Cylindrical Grinding Hard Alloys Works
An abrasive wheel removes a fine, controlled layer from the Hard Alloys part. Wheel specification, dressing interval, infeed and coolant are matched to the alloy's hardness so the surface is not burned or left with residual stress.
Programming is driven directly by your 3D model or print. Work-holding, tool selection and the cutting strategy are planned around the critical features and the material before the first chip is cut. First-off inspection confirms the process is centred before production continues.
Achievable Tolerances for CNC Cylindrical Grinding Hard Alloys
| Feature | Standard | Precision |
|---|---|---|
| Size (OD, ID, thickness) | ±0.005 mm | ±0.002 mm |
| Flatness over 100 mm | 0.010 mm | 0.003 mm |
| Parallelism | 0.010 mm | 0.003 mm |
| Roundness | 0.005 mm | 0.002 mm |
| Squareness | 0.010 mm | 0.005 mm |
| Surface finish | Ra 0.4 µm | Ra 0.1 µm |
| Workpiece hardness | up to 62 HRC | up to 65 HRC |
Standard is what a normal quotation assumes. Precision is available on nominated features and is priced separately, because it needs extra setups, in-process gauging and CMM verification. Call out only the features that need it — blanket-tightening a drawing is the single most common reason a quote comes back expensive.
Design Tips for CNC Cylindrical Grinding Hard Alloys
We are happy to suggest design tweaks that improve manufacturability. Allowing adequate grind stock, specifying realistic flatness over the true datum, and relieving corners help us hit tight tolerances on Hard Alloys efficiently. If you send your model early, we will return practical DFM feedback before you commit to production.
CNC Cylindrical Grinding Tolerances & Surface Finish
Ground Hard Alloys reaches single-micron tolerances on size, flatness and parallelism, with surface finishes down to Ra 0.1–0.4 µm — and a near-mirror finish on suitable alloys.
Exact achievable figures depend on the alloy, the feature size and the part geometry. Tell us which dimensions are critical and we will advise feasibility up front.
Applications of CNC Cylindrical Grinding Hard Alloys
Customers order CNC Cylindrical Grinding Hard Alloys components for everything from instrumentation to structural and functional assemblies. Whether you need a single prototype or recurring production volume, the same process discipline applies.
Typical Hard Alloys Parts for CNC Cylindrical Grinding
Illustrative examples of CNC Cylindrical Grinding Hard Alloys parts and the callouts that usually drive the process plan. They show the kind of work that fits this process; they are not specific customer orders.
Mould insert
- Material
- Hard Alloys
- Size
- 80 × 60 × 25 mm
- Key callouts
- Flatness 0.003 mm, squareness 0.005 mm
- Batch
- 90 pcs
Surface ground on all six faces so the insert seats without shimming.
Ceramic-coated shaft journal
- Material
- Hard Alloys
- Size
- Ø45 × 180 mm
- Key callouts
- OD ±0.003 mm, roundness 0.002 mm, Ra 0.2 µm
- Batch
- 150 pcs
Ground after coating; the coating is never the final dimension.
Lapping plate
- Material
- Hard Alloys
- Size
- 300 × 300 × 30 mm
- Key callouts
- Flatness 0.005 mm over the full face
- Batch
- 20 pcs
Ground, stress-relieved, ground again — one pass will not hold flatness on this area.
No drawing yet? Build one in the browser.
Set the metal, dimensions and features, watch the 3D model update as you type, then switch to the 2D sheet to add dimensions and tolerances. Download it or send it straight to us with your RFQ.
What We Need to Quote CNC Cylindrical Grinding Hard Alloys
- GeometrySTEP or IGES for the 3D model, plus a PDF drawing if you have tolerance callouts. A dimensioned sketch is enough to start.
- MaterialThe exact Hard Alloys grade and condition — temper, heat-treat state or hardness. If you are not sure, tell us the function and we will suggest one.
- QuantityPrototype count and the expected annual volume. Both change how the part is made and therefore what it costs.
- TolerancesWhich features are critical. Everything else runs to our standard tolerance, which is what keeps the price sensible.
- FinishSurface treatment, cosmetic requirements, and any faces that must be masked.
- DocumentsWhether you need a material certificate, dimensional report, FAIR or PPAP with the shipment.
Missing something from the list is not a problem — send what you have. We will come back with the specific questions rather than a generic form.
Other Metals for CNC Cylindrical Grinding
Other Processes for Hard Alloys
Send the drawing, the Hard Alloys grade and the quantity. You get pricing, lead time and any DFM notes back — usually within one business day.
Request a QuoteFrequently Asked Questions
Which industries use CNC Cylindrical Grinding Hard Alloys parts?
CNC Cylindrical Grinding Hard Alloys parts are used across aerospace, medical, automotive, electronics, semiconductor and general industrial sectors — anywhere precise Hard Alloys components are required.
What tolerances can you hold for CNC Cylindrical Grinding Hard Alloys?
Achievable tolerances for Hard Alloys grinding depend on the alloy, geometry and feature size. Grinding routinely holds single-micron tolerances on diameter, flatness and parallelism. Exact figures are confirmed against your drawing callouts.
Why is Hard Alloys a good choice for CNC Cylindrical Grinding?
Hard Alloys is wear-resistant carbide and hardened tool materials, which makes it well suited to CNC Cylindrical Grinding. We tune the process to the alloy so the finished Hard Alloys grinding part meets your dimensional and functional requirements.
What is CNC Cylindrical Grinding Hard Alloys and how is it done?
CNC Cylindrical Grinding Hard Alloys refers to cylindrical grinding finishes outer diameters of rotational parts to precise size and roundness. Applied to Hard Alloys — wear-resistant carbide and hardened tool materials — VT machining produces each part to your CAD drawing, selecting parameters from your tolerance, finish and quantity requirements.
What material thickness or size range suits CNC Cylindrical Grinding Hard Alloys?
We machine Hard Alloys across a broad size range; share your part envelope for confirmation.