CNC Waterjet Cutting Hard Alloys from VT machining delivers precision Hard Alloys parts produced to your exact drawing. Abrasive waterjet cutting erodes metal with a high-pressure abrasive stream, with no heat-affected zone, and we tune every parameter to the behaviour of Hard Alloys, which is wear-resistant carbide and hardened tool materials.
Process Data for CNC Waterjet Cutting Hard Alloys
| Cutting speed at 10 mm | ~13 mm/min |
|---|---|
| Cutting speed at 25 mm | ~4 mm/min |
| Profile tolerance | ±0.1 mm; edge taper <0.05 mm with taper compensation |
| Heat-affected zone | None |
Shown for Tungsten Carbide, the most common Hard Alloys grade we see for CNC Waterjet Cutting. Typical values for Tungsten Carbide, Sintered; confirmed on the first part.
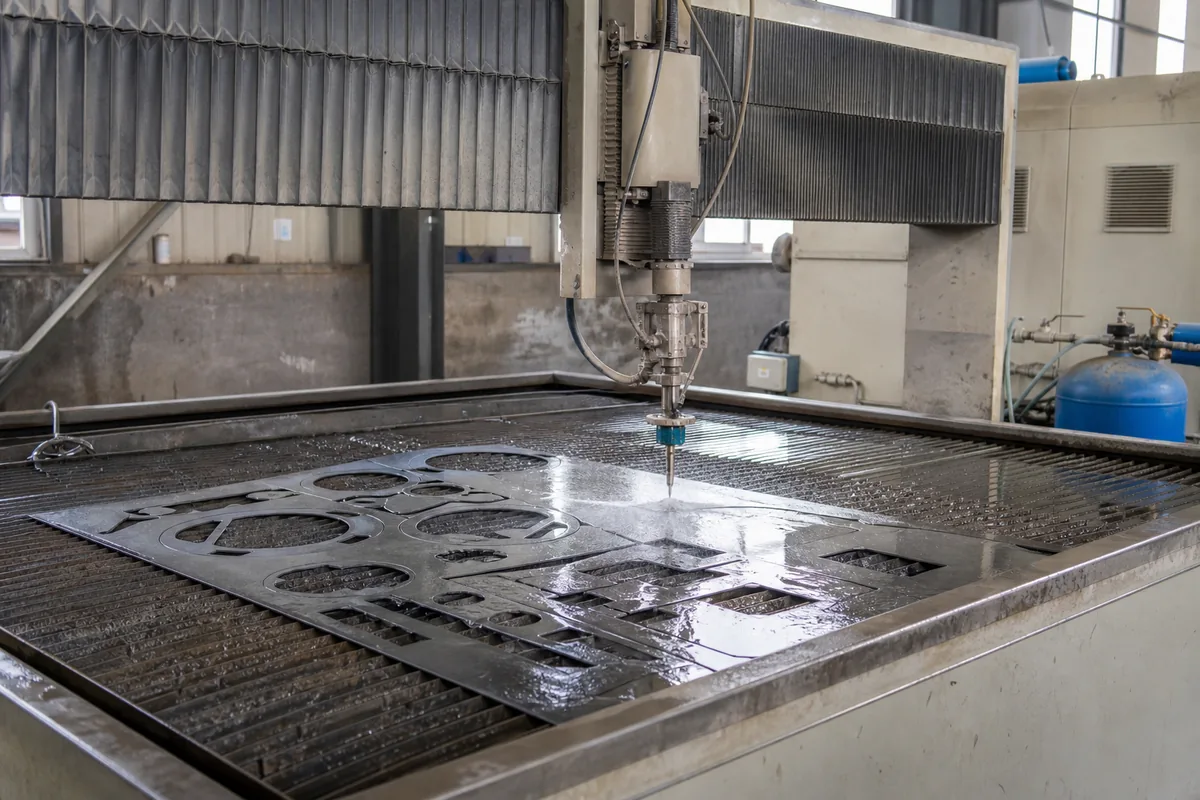
CNC Waterjet Cutting Capability for Hard Alloys
- No heat-affected zone
- Thickness to 150+ mm
- Tolerance ±0.1 mm
- Any-metal capability
Hard Alloys material properties, finishing options and grade notes are on our CNC Laser Cutting Hard Alloys page.
How CNC Waterjet Cutting Hard Alloys Works
A focused fibre-laser beam melts and blows material from the Hard Alloys sheet along the programmed contour. Power, focal position, nozzle stand-off and assist-gas pressure are tuned to the alloy and thickness for a clean, square edge.
Every job begins from your CAD model or 2D drawing. Fixturing and tool paths are planned so the most critical dimensions are produced in the most rigid, repeatable setup. Critical dimensions are checked on the first part and monitored through the run.
Achievable Tolerances for CNC Waterjet Cutting Hard Alloys
| Feature | Standard | Precision |
|---|---|---|
| Contour dimension | ±0.10 mm | ±0.05 mm |
| Hole diameter | ±0.10 mm | ±0.05 mm |
| Kerf width | 0.20 mm | 0.10 mm |
| Squareness of cut edge | 0.5° | 0.2° |
| Heat-affected zone | 0.15 mm | 0.05 mm (N₂ assist) |
| Minimum hole diameter | 1.2 × thickness | 1.0 × thickness |
| Edge condition | light dross | burr-free, N₂ cut |
Standard is what a normal quotation assumes. Precision is available on nominated features and is priced separately, because it needs extra setups, in-process gauging and CMM verification. Call out only the features that need it — blanket-tightening a drawing is the single most common reason a quote comes back expensive.
CNC Waterjet Cutting Tolerances & Surface Finish
Laser-cut Hard Alloys holds contour tolerances around ±0.05 mm depending on thickness, with a narrow kerf and a clean, near burr-free edge.
Final tolerances are governed by the material's behaviour, wall thickness and overall stiffness. We give honest DFM feedback if a callout would be costly or better achieved another way.
Design Tips for CNC Waterjet Cutting Hard Alloys
A few design choices make a real difference to cost and quality. Keeping holes no smaller than the material thickness, allowing for kerf, and grouping features sensibly improves edge quality and nesting yield on Hard Alloys. If you send your model early, we will return practical DFM feedback before you commit to production.
Applications of CNC Waterjet Cutting Hard Alloys
CNC Waterjet Cutting of Hard Alloys supports parts across aerospace, medical, automotive, electronics, semiconductor, energy and general industrial sectors. We scale from one-off prototypes to ongoing production while holding the same quality.
Typical Hard Alloys Parts for CNC Waterjet Cutting
Illustrative examples of CNC Waterjet Cutting Hard Alloys parts and the callouts that usually drive the process plan. They show the kind of work that fits this process; they are not specific customer orders.
Gasket / shim set
- Material
- Hard Alloys
- Size
- Ø120 × 0.5 mm
- Key callouts
- ID/OD ±0.05 mm, no heat discolouration
- Batch
- 3,000 pcs
Small-diameter holes below 1.2 × thickness are punched, not lased.
Machine guard panel
- Material
- Hard Alloys
- Size
- 900 × 600 × 3 mm
- Key callouts
- Slot pattern ±0.10 mm, hole-to-edge 6 mm
- Batch
- 150 pcs
Cut with common-line pairs to halve the pierce count.
Control panel face
- Material
- Hard Alloys
- Size
- 400 × 300 × 1.5 mm
- Key callouts
- Cutout position ±0.10 mm, no dross on visible face
- Batch
- 600 pcs
Cut with nitrogen so the edge takes powder coat without secondary grinding.
No drawing yet? Build one in the browser.
Set the metal, dimensions and features, watch the 3D model update as you type, then switch to the 2D sheet to add dimensions and tolerances. Download it or send it straight to us with your RFQ.
What We Need to Quote CNC Waterjet Cutting Hard Alloys
- GeometrySTEP or IGES for the 3D model, plus a PDF drawing if you have tolerance callouts. A dimensioned sketch is enough to start.
- MaterialThe exact Hard Alloys grade and condition — temper, heat-treat state or hardness. If you are not sure, tell us the function and we will suggest one.
- QuantityPrototype count and the expected annual volume. Both change how the part is made and therefore what it costs.
- TolerancesWhich features are critical. Everything else runs to our standard tolerance, which is what keeps the price sensible.
- FinishSurface treatment, cosmetic requirements, and any faces that must be masked.
- DocumentsWhether you need a material certificate, dimensional report, FAIR or PPAP with the shipment.
Missing something from the list is not a problem — send what you have. We will come back with the specific questions rather than a generic form.
Other Metals for CNC Waterjet Cutting
Other Processes for Hard Alloys
Send the drawing, the Hard Alloys grade and the quantity. You get pricing, lead time and any DFM notes back — usually within one business day.
Request a QuoteFrequently Asked Questions
Which industries use CNC Waterjet Cutting Hard Alloys parts?
CNC Waterjet Cutting Hard Alloys parts are used across aerospace, medical, automotive, electronics, semiconductor and general industrial sectors — anywhere precise Hard Alloys components are required.
What tolerances can you hold for CNC Waterjet Cutting Hard Alloys?
Achievable tolerances for Hard Alloys cutting depend on the alloy, geometry and feature size. Laser cutting holds contour tolerances to around ±0.05 mm depending on thickness. Exact figures are confirmed against your drawing callouts.
Does CNC Waterjet Cutting Hard Alloys require dedicated tooling?
Most Hard Alloys cutting work uses standard cutting tools and CNC programs; dedicated fixtures are made only when geometry or volume requires them.
What is CNC Waterjet Cutting Hard Alloys and how is it done?
CNC Waterjet Cutting Hard Alloys refers to abrasive waterjet cutting erodes metal with a high-pressure abrasive stream, with no heat-affected zone. Applied to Hard Alloys — wear-resistant carbide and hardened tool materials — VT machining produces each part to your CAD drawing, selecting parameters from your tolerance, finish and quantity requirements.
What is the typical lead time and minimum order for CNC Waterjet Cutting Hard Alloys?
CNC Waterjet Cutting prototypes for Hard Alloys can be produced quickly and scaled to series production. Send your drawing and quantity and we will advise lead time and any minimum order.
How clean are the edges produced by CNC Waterjet Cutting on Hard Alloys?
Laser cutting leaves Hard Alloys with a narrow kerf and a clean, near burr-free edge and only a small heat-affected zone.