CNC Sinker EDM Kovar is a core capability at VT machining. We combine controlled EDM machining with material-aware setup for Kovar — an alloy that is matched thermal expansion for glass/ceramic seals — to produce parts that meet your specification first time.
Process Data for CNC Sinker EDM Kovar
| Electrode | Graphite (roughing) / copper (fine finish) |
|---|---|
| Relative removal rate | Medium (vs tool steel = medium) |
| Best finish | VDI 12-18 (Ra 0.4-0.8 µm) |
Shown for Kovar, the most common Kovar grade we see for CNC Sinker EDM. Typical values for Kovar, Annealed; confirmed on the first part.
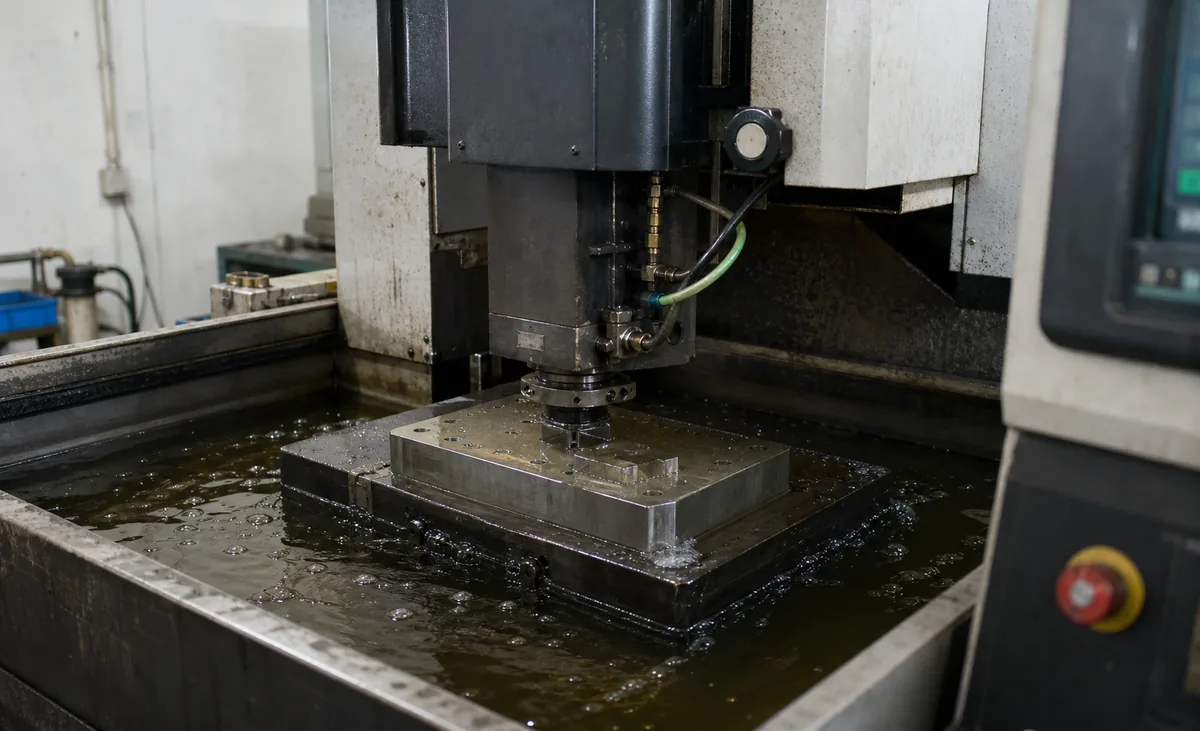
CNC Sinker EDM Capability for Kovar
- Blind cavities & ribs
- Fine surface (VDI grades)
- Tolerance to ±0.005 mm
- Hardened tool steel
Kovar material properties, finishing options and grade notes are on our CNC Wire EDM Kovar page.
How CNC Sinker EDM Kovar Works
Material is removed from the Kovar workpiece by controlled electrical discharges across a dielectric gap, with no mechanical contact. Flushing, on/off pulse timing and electrode/wire feed are set to balance speed against surface finish.
Programming is driven directly by your 3D model or print. Work-holding, tool selection and the cutting strategy are planned around the critical features and the material before the first chip is cut. First-off inspection confirms the process is centred before production continues.
Achievable Tolerances for CNC Sinker EDM Kovar
| Feature | Standard | Precision |
|---|---|---|
| Profile dimension | ±0.010 mm | ±0.002 mm |
| Internal corner radius | 0.15 mm | 0.05 mm |
| Taper control over 50 mm | 0.02 mm | 0.005 mm |
| Surface finish (skim passes) | Ra 0.8 µm | Ra 0.2 µm |
| Recast layer | 10 µm | 2 µm (fine skim) |
| Start-hole diameter | 1.0 mm | 0.25 mm |
| Workpiece hardness | no limit (conductive) | no limit (conductive) |
Standard is what a normal quotation assumes. Precision is available on nominated features and is priced separately, because it needs extra setups, in-process gauging and CMM verification. Call out only the features that need it — blanket-tightening a drawing is the single most common reason a quote comes back expensive.
Design Tips for CNC Sinker EDM Kovar
We are happy to suggest design tweaks that improve manufacturability. EDM suits sharp internal corners, thin ribs and hardened Kovar that cannot be milled; allowing a small corner radius where possible speeds the cut. If you send your model early, we will return practical DFM feedback before you commit to production.
CNC Sinker EDM Tolerances & Surface Finish
EDM holds tolerances to roughly ±0.002–0.005 mm with no cutting force on the Kovar part, producing fine, controlled surface textures and sharp internal corners impossible to mill.
Exact achievable figures depend on the alloy, the feature size and the part geometry. Tell us which dimensions are critical and we will advise feasibility up front.
Applications of CNC Sinker EDM Kovar
Customers order CNC Sinker EDM Kovar components for everything from instrumentation to structural and functional assemblies. Whether you need a single prototype or recurring production volume, the same process discipline applies.
Typical Kovar Parts for CNC Sinker EDM
Illustrative examples of CNC Sinker EDM Kovar parts and the callouts that usually drive the process plan. They show the kind of work that fits this process; they are not specific customer orders.
Spline broach section
- Material
- Kovar
- Size
- Ø28 × 40 mm
- Key callouts
- Involute profile ±0.005 mm, Ra 0.4 µm
- Batch
- 60 pcs
Wire EDM after hardening to 62 HRC — the profile would not survive being cut soft and heat-treated.
Injection mould cavity rib
- Material
- Kovar
- Size
- 0.25 mm wide × 8 mm deep
- Key callouts
- Width ±0.005 mm, VDI 21 finish
- Batch
- 45 pcs
Sinker EDM with a graphite electrode; a cutter that thin would break in the first pass.
Turbine blade fir-tree root
- Material
- Kovar
- Size
- 40 × 25 mm section
- Key callouts
- Profile ±0.008 mm
- Batch
- 120 pcs
Held on a dedicated fixture so every blade in the set indexes identically.
No drawing yet? Build one in the browser.
Set the metal, dimensions and features, watch the 3D model update as you type, then switch to the 2D sheet to add dimensions and tolerances. Download it or send it straight to us with your RFQ.
What We Need to Quote CNC Sinker EDM Kovar
- GeometrySTEP or IGES for the 3D model, plus a PDF drawing if you have tolerance callouts. A dimensioned sketch is enough to start.
- MaterialThe exact Kovar grade and condition — temper, heat-treat state or hardness. If you are not sure, tell us the function and we will suggest one.
- QuantityPrototype count and the expected annual volume. Both change how the part is made and therefore what it costs.
- TolerancesWhich features are critical. Everything else runs to our standard tolerance, which is what keeps the price sensible.
- FinishSurface treatment, cosmetic requirements, and any faces that must be masked.
- DocumentsWhether you need a material certificate, dimensional report, FAIR or PPAP with the shipment.
Missing something from the list is not a problem — send what you have. We will come back with the specific questions rather than a generic form.
Other Metals for CNC Sinker EDM
Other Processes for Kovar
Send the drawing, the Kovar grade and the quantity. You get pricing, lead time and any DFM notes back — usually within one business day.
Request a QuoteFrequently Asked Questions
Can VT machining make custom Kovar parts to my drawing?
Yes. Kovar EDM machining is made to order from your CAD/2D drawing. Share your geometry, material grade, tolerance and quantity and we will confirm feasibility, lead time and pricing.
What is CNC Sinker EDM Kovar and how is it done?
CNC Sinker EDM Kovar refers to sinker (die-sink) EDM burns a shaped electrode into metal to form precise cavities and blind features. Applied to Kovar — matched thermal expansion for glass/ceramic seals — VT machining produces each part to your CAD drawing, selecting parameters from your tolerance, finish and quantity requirements.
Which industries use CNC Sinker EDM Kovar parts?
CNC Sinker EDM Kovar parts are used across aerospace, medical, automotive, electronics, semiconductor and general industrial sectors — anywhere precise Kovar components are required.
What tolerances can you hold for CNC Sinker EDM Kovar?
Achievable tolerances for Kovar EDM machining depend on the alloy, geometry and feature size. EDM holds tolerances to around ±0.002 mm with no cutting force on the part. Exact figures are confirmed against your drawing callouts.
Does CNC Sinker EDM Kovar require dedicated tooling?
Wire EDM needs no shaped tooling; sinker EDM uses a shaped electrode we produce in-house for your cavity.