VT machining provides CNC Gear Hobbing Phosphor Bronze for customers who need accurate, repeatable Phosphor Bronze components. Because Phosphor Bronze is springy, wear and corrosion resistant, we adapt the process to suit — controlling the variables that matter for this alloy.
Process Data for CNC Gear Hobbing Phosphor Bronze
| Heat-treat route | None (used as supplied) |
|---|---|
| Accuracy as cut | ISO 1328 class 8-9 (AGMA 9-10) |
| Module range | 0.3-6 |
| Hobbing speed (HSS-E / carbide) | 30 / 95 m/min |
| Hob | HSS-E (PM) coated hob; carbide for dry hobbing |
| Gear types | External spur and helical, splines, worm wheels |
Shown for C510 Phosphor Bronze, the most common Phosphor Bronze grade we see for CNC Gear Hobbing. Typical values for C510 Phosphor Bronze, Spring temper; confirmed on the first part.
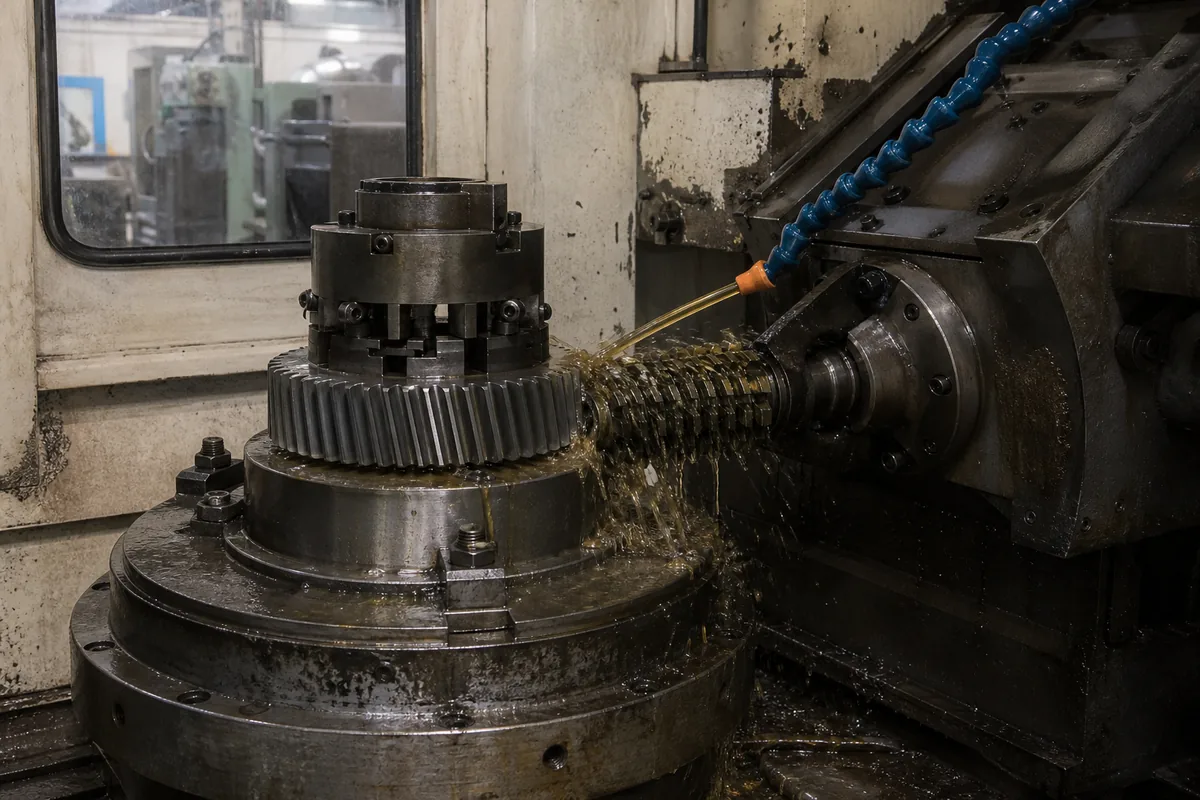
CNC Gear Hobbing Capability for Phosphor Bronze
- Spur & helical gears
- Module range support
- Pre-grind accuracy
- High productivity
Phosphor Bronze Material Data
| Density | 8.86 g/cm³ |
|---|---|
| Tensile strength | 325–965 MPa |
| Yield strength (0.2%) | 140–550 MPa |
| Hardness | 60–200 HV |
| Melting point | 975–1060 °C |
| Thermal conductivity | 69 W/m·K |
| Thermal expansion | 17.8 ×10⁻⁶/K |
| Electrical conductivity | 15% |
| Machinability (C36000 = 100%) | 20% |
| Grades we run | C51000, C51900, C52100, C54400 free-cutting |
Published typical values for C51000. Other grades in the family differ — the certificate supplied with your order carries the actual heat-lot figures.
Spring temper is destroyed by heat. Contacts and spring fingers are etched or wire-EDM cut, never laser cut.
How CNC Gear Hobbing Phosphor Bronze Works
Tooth profiles are generated in the Phosphor Bronze blank by a synchronised cutter, then refined to the required accuracy class. Module, pressure angle and helix are programmed from your gear data.
We start from your supplied geometry and tolerance scheme. The setup is designed to minimise re-clamping, which protects positional accuracy across features. A first article is verified against the drawing before the balance of the batch is released.
Achievable Tolerances for CNC Gear Hobbing Phosphor Bronze
| Feature | Standard | Precision |
|---|---|---|
| Accuracy class | DIN 8 / AGMA 10 | DIN 6 / AGMA 12 |
| Profile deviation | 0.020 mm | 0.008 mm |
| Lead deviation | 0.020 mm | 0.008 mm |
| Pitch deviation (cumulative) | 0.040 mm | 0.015 mm |
| Runout | 0.030 mm | 0.010 mm |
| Tooth surface finish | Ra 1.6 µm | Ra 0.4 µm (ground) |
| Module range | m0.5–m8 | m1–m6 |
Standard is what a normal quotation assumes. Precision is available on nominated features and is priced separately, because it needs extra setups, in-process gauging and CMM verification. Call out only the features that need it — blanket-tightening a drawing is the single most common reason a quote comes back expensive.
Design Tips for CNC Gear Hobbing Phosphor Bronze
Small design adjustments often cut cost and lead time. Providing complete gear data (module, pressure angle, profile shift, quality class) lets us produce Phosphor Bronze gears right the first time. If you send your model early, we will return practical DFM feedback before you commit to production.
Working with Phosphor Bronze
Phosphor Bronze is springy, wear and corrosion resistant. We translate those properties into a process plan: the right tooling, speeds, feeds and fixturing for the alloy.
Where the grade, temper or heat-treat condition matters to performance, we confirm it with you and can supply material certificates. Material is procured to recognised standards for consistent, repeatable results.
CNC Gear Hobbing Tolerances & Surface Finish
Gear features are produced to a specified DIN/AGMA accuracy class, with profile and lead controlled for quiet, durable running under load.
The tightest tolerances are reserved for the features your drawing flags as critical. Share your tolerance scheme and we will confirm what is realistic before quoting.
Applications of CNC Gear Hobbing Phosphor Bronze
Phosphor Bronze parts made this way are found throughout aerospace, medical, automotive, electronics and industrial equipment. Prototype, bridge and production volumes are all welcome.
Typical Phosphor Bronze Parts for CNC Gear Hobbing
Illustrative examples of CNC Gear Hobbing Phosphor Bronze parts and the callouts that usually drive the process plan. They show the kind of work that fits this process; they are not specific customer orders.
Spur gear
- Material
- Phosphor Bronze
- Size
- m2, z40, 20° PA, face 20 mm
- Key callouts
- DIN 7, runout 0.02 mm
- Batch
- 500 pcs
Hobbed, hardened, then hard-finished; skipping the finish pass costs a full accuracy class.
Bevel gear pair
- Material
- Phosphor Bronze
- Size
- m2, z20/z40, 90° axes
- Key callouts
- DIN 8, mounting distance ±0.03 mm
- Batch
- 200 sets
Contact pattern checked on a rolling tester before release.
Splined shaft
- Material
- Phosphor Bronze
- Size
- DIN 5480, 26 × 1.5
- Key callouts
- Fit class H7/g6, runout 0.02 mm
- Batch
- 800 pcs
Spline hobbed with the journals ground afterwards on the same centres.
Finishing Options for Phosphor Bronze
| Finish | Thickness / effect | Why it gets specified |
|---|---|---|
| Deburr / edge break | 0.05–0.3 mm | All parts unless the drawing says otherwise |
| Bead blast | Ra 1.6–3.2 µm | Uniform matt finish, hides tool marks |
| Laser marking | — | Part number, lot code, data matrix |
No drawing yet? Build one in the browser.
Set the metal, dimensions and features, watch the 3D model update as you type, then switch to the 2D sheet to add dimensions and tolerances. Download it or send it straight to us with your RFQ.
What We Need to Quote CNC Gear Hobbing Phosphor Bronze
- GeometrySTEP or IGES for the 3D model, plus a PDF drawing if you have tolerance callouts. A dimensioned sketch is enough to start.
- MaterialThe exact Phosphor Bronze grade and condition — temper, heat-treat state or hardness. If you are not sure, tell us the function and we will suggest one.
- QuantityPrototype count and the expected annual volume. Both change how the part is made and therefore what it costs.
- TolerancesWhich features are critical. Everything else runs to our standard tolerance, which is what keeps the price sensible.
- FinishSurface treatment, cosmetic requirements, and any faces that must be masked.
- DocumentsWhether you need a material certificate, dimensional report, FAIR or PPAP with the shipment.
Missing something from the list is not a problem — send what you have. We will come back with the specific questions rather than a generic form.
Other Metals for CNC Gear Hobbing
Other Processes for Phosphor Bronze
Send the drawing, the Phosphor Bronze grade and the quantity. You get pricing, lead time and any DFM notes back — usually within one business day.
Request a QuoteFrequently Asked Questions
Does CNC Gear Hobbing Phosphor Bronze require dedicated tooling?
Most Phosphor Bronze gear cutting work uses standard cutting tools and CNC programs; dedicated fixtures are made only when geometry or volume requires them.
What material thickness or size range suits CNC Gear Hobbing Phosphor Bronze?
We machine Phosphor Bronze across a broad size range; share your part envelope for confirmation.
How clean are the edges produced by CNC Gear Hobbing on Phosphor Bronze?
Machined Phosphor Bronze edges are clean and to specification; edge-break or deburring is added when your drawing calls for it.
What is CNC Gear Hobbing Phosphor Bronze and how is it done?
CNC Gear Hobbing Phosphor Bronze refers to gear hobbing generates gear teeth with a rotating hob synchronized to the workpiece. Applied to Phosphor Bronze — springy, wear and corrosion resistant — VT machining produces each part to your CAD drawing, selecting parameters from your tolerance, finish and quantity requirements.