CNC EDM Drilling Inconel from VT machining delivers precision Inconel parts produced to your exact drawing. Fast-hole EDM drilling produces small, deep holes in hard metals, including starter holes for wire EDM, and we tune every parameter to the behaviour of Inconel, which is high-temperature strength and oxidation resistance.
Process Data for CNC EDM Drilling Inconel
| Hole diameter range | Ø0.3-3.0 mm |
|---|---|
| Max depth-to-diameter | up to ~100:1 |
| Drilling speed, Ø1 mm | ~18 mm/min |
Shown for Inconel 718, the most common Inconel grade we see for CNC EDM Drilling. Typical values for Inconel 718, Solution-treated or aged; confirmed on the first part.
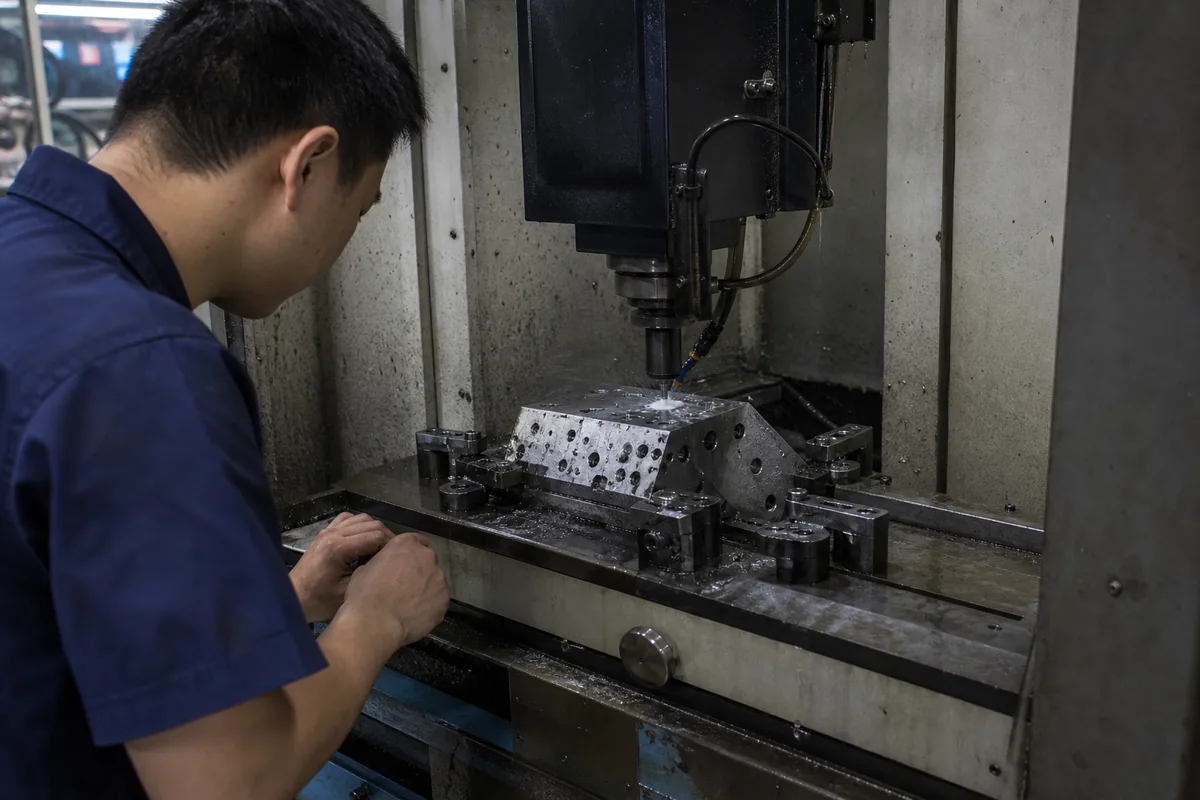
CNC EDM Drilling Capability for Inconel
- Ø0.2–3 mm holes
- Deep aspect ratios
- Hardened-metal drilling
- Angled hole capability
Inconel material properties, finishing options and grade notes are on our CNC Wire EDM Inconel page.
How CNC EDM Drilling Inconel Works
Material is removed from the Inconel workpiece by controlled electrical discharges across a dielectric gap, with no mechanical contact. Flushing, on/off pulse timing and electrode/wire feed are set to balance speed against surface finish.
We start from your supplied geometry and tolerance scheme. The setup is designed to minimise re-clamping, which protects positional accuracy across features. A first article is verified against the drawing before the balance of the batch is released.
Achievable Tolerances for CNC EDM Drilling Inconel
| Feature | Standard | Precision |
|---|---|---|
| Profile dimension | ±0.010 mm | ±0.002 mm |
| Internal corner radius | 0.15 mm | 0.05 mm |
| Taper control over 50 mm | 0.02 mm | 0.005 mm |
| Surface finish (skim passes) | Ra 0.8 µm | Ra 0.2 µm |
| Recast layer | 10 µm | 2 µm (fine skim) |
| Start-hole diameter | 1.0 mm | 0.25 mm |
| Workpiece hardness | no limit (conductive) | no limit (conductive) |
Standard is what a normal quotation assumes. Precision is available on nominated features and is priced separately, because it needs extra setups, in-process gauging and CMM verification. Call out only the features that need it — blanket-tightening a drawing is the single most common reason a quote comes back expensive.
Design Tips for CNC EDM Drilling Inconel
Small design adjustments often cut cost and lead time. EDM suits sharp internal corners, thin ribs and hardened Inconel that cannot be milled; allowing a small corner radius where possible speeds the cut. If you send your model early, we will return practical DFM feedback before you commit to production.
CNC EDM Drilling Tolerances & Surface Finish
EDM holds tolerances to roughly ±0.002–0.005 mm with no cutting force on the Inconel part, producing fine, controlled surface textures and sharp internal corners impossible to mill.
The tightest tolerances are reserved for the features your drawing flags as critical. Share your tolerance scheme and we will confirm what is realistic before quoting.
Applications of CNC EDM Drilling Inconel
Inconel parts made this way are found throughout aerospace, medical, automotive, electronics and industrial equipment. Prototype, bridge and production volumes are all welcome.
Typical Inconel Parts for CNC EDM Drilling
Illustrative examples of CNC EDM Drilling Inconel parts and the callouts that usually drive the process plan. They show the kind of work that fits this process; they are not specific customer orders.
Micro slot in nozzle
- Material
- Inconel
- Size
- 0.15 mm wide × 6 mm deep
- Key callouts
- Width ±0.003 mm
- Batch
- 400 pcs
Cut with 0.1 mm wire; the start hole is EDM-drilled at Ø0.3 mm.
Carbide punch
- Material
- Inconel
- Size
- Ø6 × 45 mm
- Key callouts
- OD ±0.003 mm, sharp form retained
- Batch
- 250 pcs
Carbide is EDM or grind only; there is no milling route.
Spline broach section
- Material
- Inconel
- Size
- Ø28 × 40 mm
- Key callouts
- Involute profile ±0.005 mm, Ra 0.4 µm
- Batch
- 60 pcs
Wire EDM after hardening to 62 HRC — the profile would not survive being cut soft and heat-treated.
No drawing yet? Build one in the browser.
Set the metal, dimensions and features, watch the 3D model update as you type, then switch to the 2D sheet to add dimensions and tolerances. Download it or send it straight to us with your RFQ.
What We Need to Quote CNC EDM Drilling Inconel
- GeometrySTEP or IGES for the 3D model, plus a PDF drawing if you have tolerance callouts. A dimensioned sketch is enough to start.
- MaterialThe exact Inconel grade and condition — temper, heat-treat state or hardness. If you are not sure, tell us the function and we will suggest one.
- QuantityPrototype count and the expected annual volume. Both change how the part is made and therefore what it costs.
- TolerancesWhich features are critical. Everything else runs to our standard tolerance, which is what keeps the price sensible.
- FinishSurface treatment, cosmetic requirements, and any faces that must be masked.
- DocumentsWhether you need a material certificate, dimensional report, FAIR or PPAP with the shipment.
Missing something from the list is not a problem — send what you have. We will come back with the specific questions rather than a generic form.
Other Metals for CNC EDM Drilling
Other Processes for Inconel
Send the drawing, the Inconel grade and the quantity. You get pricing, lead time and any DFM notes back — usually within one business day.
Request a QuoteFrequently Asked Questions
What tolerances can you hold for CNC EDM Drilling Inconel?
Achievable tolerances for Inconel EDM machining depend on the alloy, geometry and feature size. EDM holds tolerances to around ±0.002 mm with no cutting force on the part. Exact figures are confirmed against your drawing callouts.
What is CNC EDM Drilling Inconel and how is it done?
CNC EDM Drilling Inconel refers to fast-hole EDM drilling produces small, deep holes in hard metals, including starter holes for wire EDM. Applied to Inconel — high-temperature strength and oxidation resistance — VT machining produces each part to your CAD drawing, selecting parameters from your tolerance, finish and quantity requirements.
Why is Inconel a good choice for CNC EDM Drilling?
Inconel is high-temperature strength and oxidation resistance, which makes it well suited to CNC EDM Drilling. We tune the process to the alloy so the finished Inconel EDM machining part meets your dimensional and functional requirements.
What surface finish is achievable on Inconel with CNC EDM Drilling?
Surface finish on Inconel is controlled to your specification; we confirm the achievable Ra against your callout.