Looking for reliable CNC Bending Brass? VT machining manufactures Brass parts to tight tolerances and consistent quality. Brass is free-machining, good conductivity, attractive finish, so the process is set up specifically for the material.
Process Data for CNC Bending Brass
| Minimum inside bend radius | ~1 × t (across the grain) |
|---|---|
| Press force, 2 mm sheet, V16 die | ~14.7 t per metre |
| Typical springback at 90° | 1-2° |
| Angle tolerance | ±0.5° (CNC back-gauge, angle measurement on first part) |
Shown for C360 Brass, the most common Brass grade we see for CNC Bending. Typical values for C360 Brass, Half-hard; confirmed on the first part.
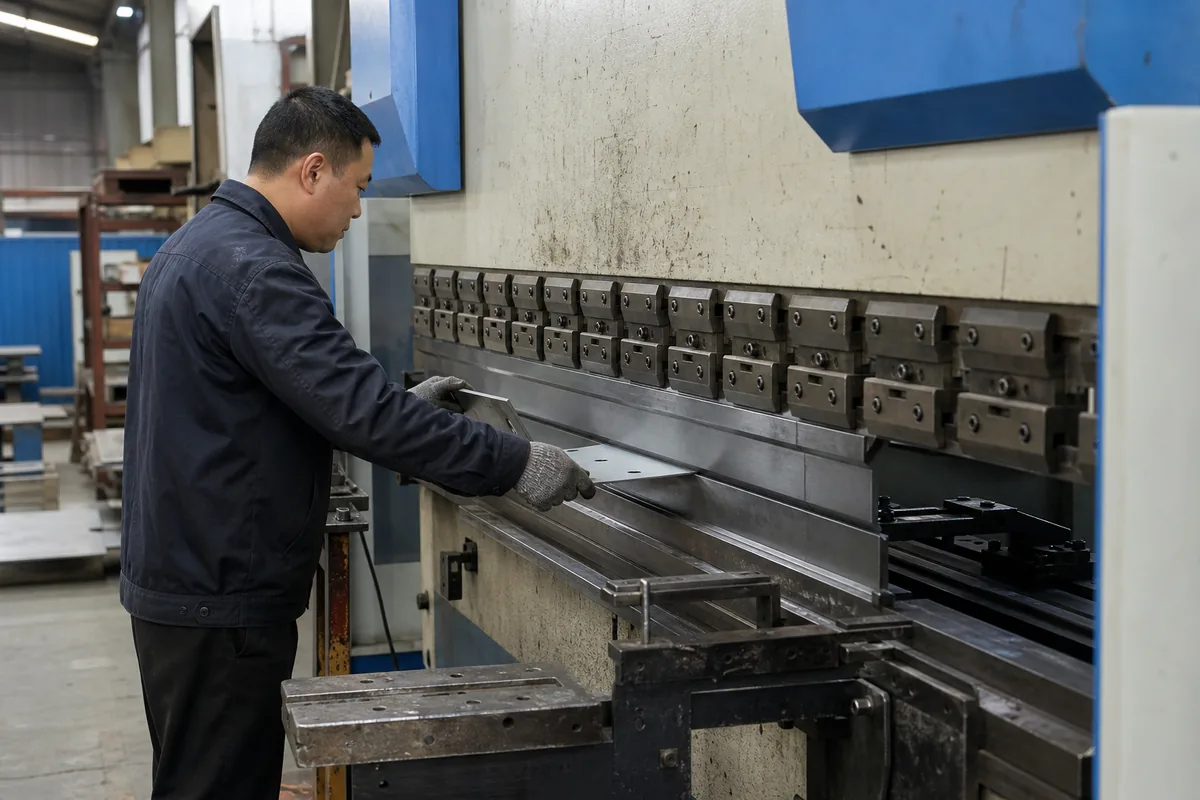
CNC Bending Capability for Brass
- Angle accuracy ±0.5°
- Back-gauge positioning
- Bend allowance control
- Multi-bend sequencing
Brass Material Data
| Density | 8.50 g/cm³ |
|---|---|
| Tensile strength | 340–470 MPa |
| Yield strength (0.2%) | 125–310 MPa |
| Hardness | 78–130 HB |
| Melting point | 885–900 °C |
| Thermal conductivity | 115 W/m·K |
| Thermal expansion | 20.5 ×10⁻⁶/K |
| Electrical conductivity | 26% |
| Machinability (C36000 = 100%) | 100% (the benchmark) |
| Grades we run | C36000 free-cutting, C37700 forging, C26000 cartridge, C46400 naval |
Published typical values for C36000. Other grades in the family differ — the certificate supplied with your order carries the actual heat-lot figures.
Nothing much — this is the easiest metal in the shop. Worth asking about if a copper or bronze part is cost-driven rather than conductivity-driven.
How CNC Bending Brass Works
The Brass blank is bent or formed against tooling under CNC-controlled ram travel and back-gauge positioning. Bend allowance and springback are compensated in the program so finished angles hit the print.
Every job begins from your CAD model or 2D drawing. Fixturing and tool paths are planned so the most critical dimensions are produced in the most rigid, repeatable setup. Critical dimensions are checked on the first part and monitored through the run.
Achievable Tolerances for CNC Bending Brass
| Feature | Standard | Precision |
|---|---|---|
| Bend angle | ±1.0° | ±0.5° |
| Flange length | ±0.30 mm | ±0.15 mm |
| Hole-to-bend distance | ±0.30 mm | ±0.15 mm |
| Minimum inside radius | 1.0 × thickness | 0.8 × thickness |
| Minimum flange height | 4 × thickness + radius | 3 × thickness + radius |
| Bend-to-bend spacing | ±0.30 mm | ±0.15 mm |
| Sheet thickness range | 0.5–8.0 mm | 0.5–4.0 mm |
Standard is what a normal quotation assumes. Precision is available on nominated features and is priced separately, because it needs extra setups, in-process gauging and CMM verification. Call out only the features that need it — blanket-tightening a drawing is the single most common reason a quote comes back expensive.
Working with Brass
Brass offers a useful combination of properties: it is free-machining, good conductivity, attractive finish. Those characteristics shape how we approach forming — from tool and parameter selection to work-holding and coolant.
If your application is sensitive to alloy condition, we agree the specification in writing and document it. Stock is sourced from reputable suppliers so what you order is what you receive.
Design Tips for CNC Bending Brass
A few design choices make a real difference to cost and quality. Consistent bend radii, adequate flange lengths and grain-direction awareness reduce cracking and springback in formed Brass. If you send your model early, we will return practical DFM feedback before you commit to production.
CNC Bending Tolerances & Surface Finish
Formed Brass holds bend angles to about ±0.5° and consistent flange dimensions, with bend allowance compensated for the material and thickness.
Final tolerances are governed by the material's behaviour, wall thickness and overall stiffness. We give honest DFM feedback if a callout would be costly or better achieved another way.
Applications of CNC Bending Brass
CNC Bending of Brass supports parts across aerospace, medical, automotive, electronics, semiconductor, energy and general industrial sectors. We scale from one-off prototypes to ongoing production while holding the same quality.
Typical Brass Parts for CNC Bending
Illustrative examples of CNC Bending Brass parts and the callouts that usually drive the process plan. They show the kind of work that fits this process; they are not specific customer orders.
U-channel
- Material
- Brass
- Size
- 800 mm long, 3 mm thick
- Key callouts
- Angle ±0.5°, straightness 1 mm over length
- Batch
- 250 pcs
Formed in two hits with a rotating die to avoid marking the outside face.
Hemmed panel edge
- Material
- Brass
- Size
- 400 mm hem, 1.2 mm
- Key callouts
- Hem flat to 0.3 mm
- Batch
- 1,500 pcs
Hemmed to remove the sharp edge without a secondary deburr operation.
Radiused cover
- Material
- Brass
- Size
- R150 × 500 mm
- Key callouts
- Radius ±1 mm, no tool marks
- Batch
- 200 pcs
Bumped in 14 small steps rather than rolled, because the batch does not justify a roll set.
Finishing Options for Brass
| Finish | Thickness / effect | Why it gets specified |
|---|---|---|
| Nickel plate | 5–15 µm | Hard, bright, corrosion resistant |
| Chrome plate | 0.3–1 µm | Decorative, over nickel |
| Clear lacquer | 10–20 µm | Stops the natural tarnish |
| Tin plate | 3–15 µm | Solderable contacts |
| Deburr / edge break | 0.05–0.3 mm | All parts unless the drawing says otherwise |
| Bead blast | Ra 1.6–3.2 µm | Uniform matt finish, hides tool marks |
| Laser marking | — | Part number, lot code, data matrix |
No drawing yet? Build one in the browser.
Set the metal, dimensions and features, watch the 3D model update as you type, then switch to the 2D sheet to add dimensions and tolerances. Download it or send it straight to us with your RFQ.
What We Need to Quote CNC Bending Brass
- GeometrySTEP or IGES for the 3D model, plus a PDF drawing if you have tolerance callouts. A dimensioned sketch is enough to start.
- MaterialThe exact Brass grade and condition — temper, heat-treat state or hardness. If you are not sure, tell us the function and we will suggest one.
- QuantityPrototype count and the expected annual volume. Both change how the part is made and therefore what it costs.
- TolerancesWhich features are critical. Everything else runs to our standard tolerance, which is what keeps the price sensible.
- FinishSurface treatment, cosmetic requirements, and any faces that must be masked.
- DocumentsWhether you need a material certificate, dimensional report, FAIR or PPAP with the shipment.
Missing something from the list is not a problem — send what you have. We will come back with the specific questions rather than a generic form.
Other Metals for CNC Bending
Other Processes for Brass
Send the drawing, the Brass grade and the quantity. You get pricing, lead time and any DFM notes back — usually within one business day.
Request a QuoteFrequently Asked Questions
What material thickness or size range suits CNC Bending Brass?
We form Brass sheet and plate to your developed flat pattern and bend sequence.
Does CNC Bending Brass require dedicated tooling?
Most Brass forming work uses standard cutting tools and CNC programs; dedicated fixtures are made only when geometry or volume requires them.
How clean are the edges produced by CNC Bending on Brass?
Machined Brass edges are clean and to specification; edge-break or deburring is added when your drawing calls for it.
Which industries use CNC Bending Brass parts?
CNC Bending Brass parts are used across aerospace, medical, automotive, electronics, semiconductor and general industrial sectors — anywhere precise Brass components are required.
What tolerances can you hold for CNC Bending Brass?
Achievable tolerances for Brass forming depend on the alloy, geometry and feature size. We hold tight, repeatable tolerances appropriate to the feature and material. Exact figures are confirmed against your drawing callouts.
What is the typical lead time and minimum order for CNC Bending Brass?
CNC Bending prototypes for Brass can be produced quickly and scaled to series production. Send your drawing and quantity and we will advise lead time and any minimum order.