VT machining provides CNC 4-Axis Machining Stainless Steel for customers who need accurate, repeatable Stainless Steel components. Because Stainless Steel is corrosion resistant, strong, hygienic (304/316 grades), we adapt the process to suit — controlling the variables that matter for this alloy.
Starting Parameters for CNC 4-Axis Machining Stainless Steel
| Cutting speed (carbide) | 95-175 m/min |
|---|---|
| Feed per tooth | 0.028-0.088 mm |
| Spindle speed, Ø10 mm end mill | 3020-5570 rpm |
| Insert / tool class | ISO M — positive-rake PVD/CVD carbide |
| Coolant | Flood emulsion (8-10%) or high-pressure coolant |
| Rotary positioning accuracy | ±10 arc-sec (≈ ±0.005 mm at Ø100 mm) |
Shown for 304 Stainless Steel, the most common Stainless Steel grade we see for CNC 4-Axis Machining. Starting values for 304 Stainless Steel, Annealed; optimised on the first article.
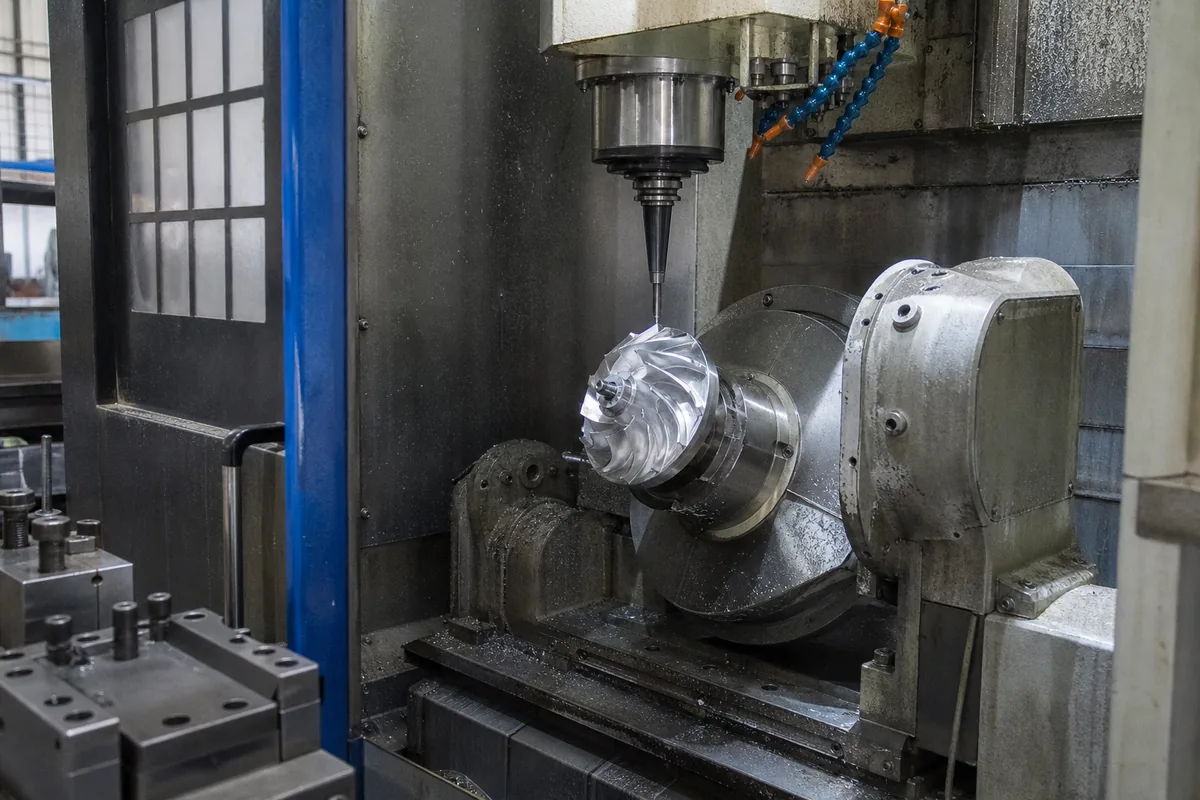
CNC 4-Axis Machining Capability for Stainless Steel
- Indexed & continuous 4th axis
- Multi-face in one setup
- Tolerance to ±0.01 mm
- Rotary fixturing
Stainless Steel material properties, finishing options and grade notes are on our CNC Milling Stainless Steel page.
How CNC 4-Axis Machining Stainless Steel Works
Rotating multi-flute cutters remove material as the Stainless Steel workpiece is driven through programmed tool paths on 3-, 4- or 5-axis machining centres. Climb milling, step-over and depth-of-cut are set so chip load stays in the ideal band for the alloy.
Every job begins from your CAD model or 2D drawing. Fixturing and tool paths are planned so the most critical dimensions are produced in the most rigid, repeatable setup. Critical dimensions are checked on the first part and monitored through the run.
Achievable Tolerances for CNC 4-Axis Machining Stainless Steel
| Feature | Standard | Precision |
|---|---|---|
| Linear dimension (< 100 mm) | ±0.05 mm | ±0.010 mm |
| Linear dimension (100–300 mm) | ±0.10 mm | ±0.025 mm |
| Hole diameter (reamed) | H9 | H7 |
| True position of hole pattern | ±0.10 mm | ±0.025 mm |
| Flatness over 100 mm | 0.05 mm | 0.015 mm |
| Perpendicularity | 0.10 mm | 0.020 mm |
| Surface finish, as machined | Ra 1.6 µm | Ra 0.4 µm |
Standard is what a normal quotation assumes. Precision is available on nominated features and is priced separately, because it needs extra setups, in-process gauging and CMM verification. Call out only the features that need it — blanket-tightening a drawing is the single most common reason a quote comes back expensive.
Design Tips for CNC 4-Axis Machining Stainless Steel
A few design choices make a real difference to cost and quality. Generous internal radii, sensible pocket depth-to-width ratios and avoiding very thin unsupported walls all reduce cost and improve accuracy in Stainless Steel. If you send your model early, we will return practical DFM feedback before you commit to production.
CNC 4-Axis Machining Tolerances & Surface Finish
For CNC 4-Axis Machining, dimensional and positional tolerances around ±0.01 mm are routine, tightening toward ±0.005 mm on precision setups. Surface finish on machined faces typically falls in the Ra 0.4–1.6 µm range depending on tooling and pass strategy.
Final tolerances are governed by the material's behaviour, wall thickness and overall stiffness. We give honest DFM feedback if a callout would be costly or better achieved another way.
Applications of CNC 4-Axis Machining Stainless Steel
CNC 4-Axis Machining of Stainless Steel supports parts across aerospace, medical, automotive, electronics, semiconductor, energy and general industrial sectors. We scale from one-off prototypes to ongoing production while holding the same quality.
Typical Stainless Steel Parts for CNC 4-Axis Machining
Illustrative examples of CNC 4-Axis Machining Stainless Steel parts and the callouts that usually drive the process plan. They show the kind of work that fits this process; they are not specific customer orders.
Manifold block
- Material
- Stainless Steel
- Size
- 120 × 60 × 45 mm
- Key callouts
- Cross-bore intersection ±0.05 mm, ports G1/8", leak-tested to 10 bar
- Batch
- 80 pcs
Deburred internally with a brush tool; a burr at a cross-bore is what fails the leak test.
Heat sink base
- Material
- Stainless Steel
- Size
- 200 × 100 × 8 mm
- Key callouts
- Fin thickness 1.2 ±0.05 mm, base flatness 0.03 mm
- Batch
- 500 pcs
Fins cut with a slotting cutter in one pass to avoid the deflection a step-over leaves.
Optical mount plate
- Material
- Stainless Steel
- Size
- 160 × 160 × 12 mm
- Key callouts
- Hole pattern true position ±0.02 mm, flatness 0.01 mm
- Batch
- 40 pcs
Roughed, stress-relieved overnight, then finished — the plate is too thin to hold flatness in one hit.
No drawing yet? Build one in the browser.
Set the metal, dimensions and features, watch the 3D model update as you type, then switch to the 2D sheet to add dimensions and tolerances. Download it or send it straight to us with your RFQ.
What We Need to Quote CNC 4-Axis Machining Stainless Steel
- GeometrySTEP or IGES for the 3D model, plus a PDF drawing if you have tolerance callouts. A dimensioned sketch is enough to start.
- MaterialThe exact Stainless Steel grade and condition — temper, heat-treat state or hardness. If you are not sure, tell us the function and we will suggest one.
- QuantityPrototype count and the expected annual volume. Both change how the part is made and therefore what it costs.
- TolerancesWhich features are critical. Everything else runs to our standard tolerance, which is what keeps the price sensible.
- FinishSurface treatment, cosmetic requirements, and any faces that must be masked.
- DocumentsWhether you need a material certificate, dimensional report, FAIR or PPAP with the shipment.
Missing something from the list is not a problem — send what you have. We will come back with the specific questions rather than a generic form.
Other Metals for CNC 4-Axis Machining
Other Processes for Stainless Steel
Send the drawing, the Stainless Steel grade and the quantity. You get pricing, lead time and any DFM notes back — usually within one business day.
Request a QuoteFrequently Asked Questions
What is the typical lead time and minimum order for CNC 4-Axis Machining Stainless Steel?
CNC 4-Axis Machining prototypes for Stainless Steel can be produced quickly and scaled to series production. Send your drawing and quantity and we will advise lead time and any minimum order.
Why is Stainless Steel a good choice for CNC 4-Axis Machining?
Stainless Steel is corrosion resistant, strong, hygienic (304/316 grades), which makes it well suited to CNC 4-Axis Machining. We tune the process to the alloy so the finished Stainless Steel machining part meets your dimensional and functional requirements.
What material thickness or size range suits CNC 4-Axis Machining Stainless Steel?
We machine Stainless Steel across a broad size range; share your part envelope for confirmation.
Which industries use CNC 4-Axis Machining Stainless Steel parts?
CNC 4-Axis Machining Stainless Steel parts are used across aerospace, medical, automotive, electronics, semiconductor and general industrial sectors — anywhere precise Stainless Steel components are required.
Can VT machining make custom Stainless Steel parts to my drawing?
Yes. Stainless Steel machining is made to order from your CAD/2D drawing. Share your geometry, material grade, tolerance and quantity and we will confirm feasibility, lead time and pricing.
What is CNC 4-Axis Machining Stainless Steel and how is it done?
CNC 4-Axis Machining Stainless Steel refers to four-axis machining adds a rotary axis for indexed or continuous machining around a part. Applied to Stainless Steel — corrosion resistant, strong, hygienic (304/316 grades) — VT machining produces each part to your CAD drawing, selecting parameters from your tolerance, finish and quantity requirements.